How do you read performance parameters: from detection to project selection
Understand how solids content, viscosity, pot life, adhesion, abrasion resistance, weatherability and chemical resistance affect material selection.
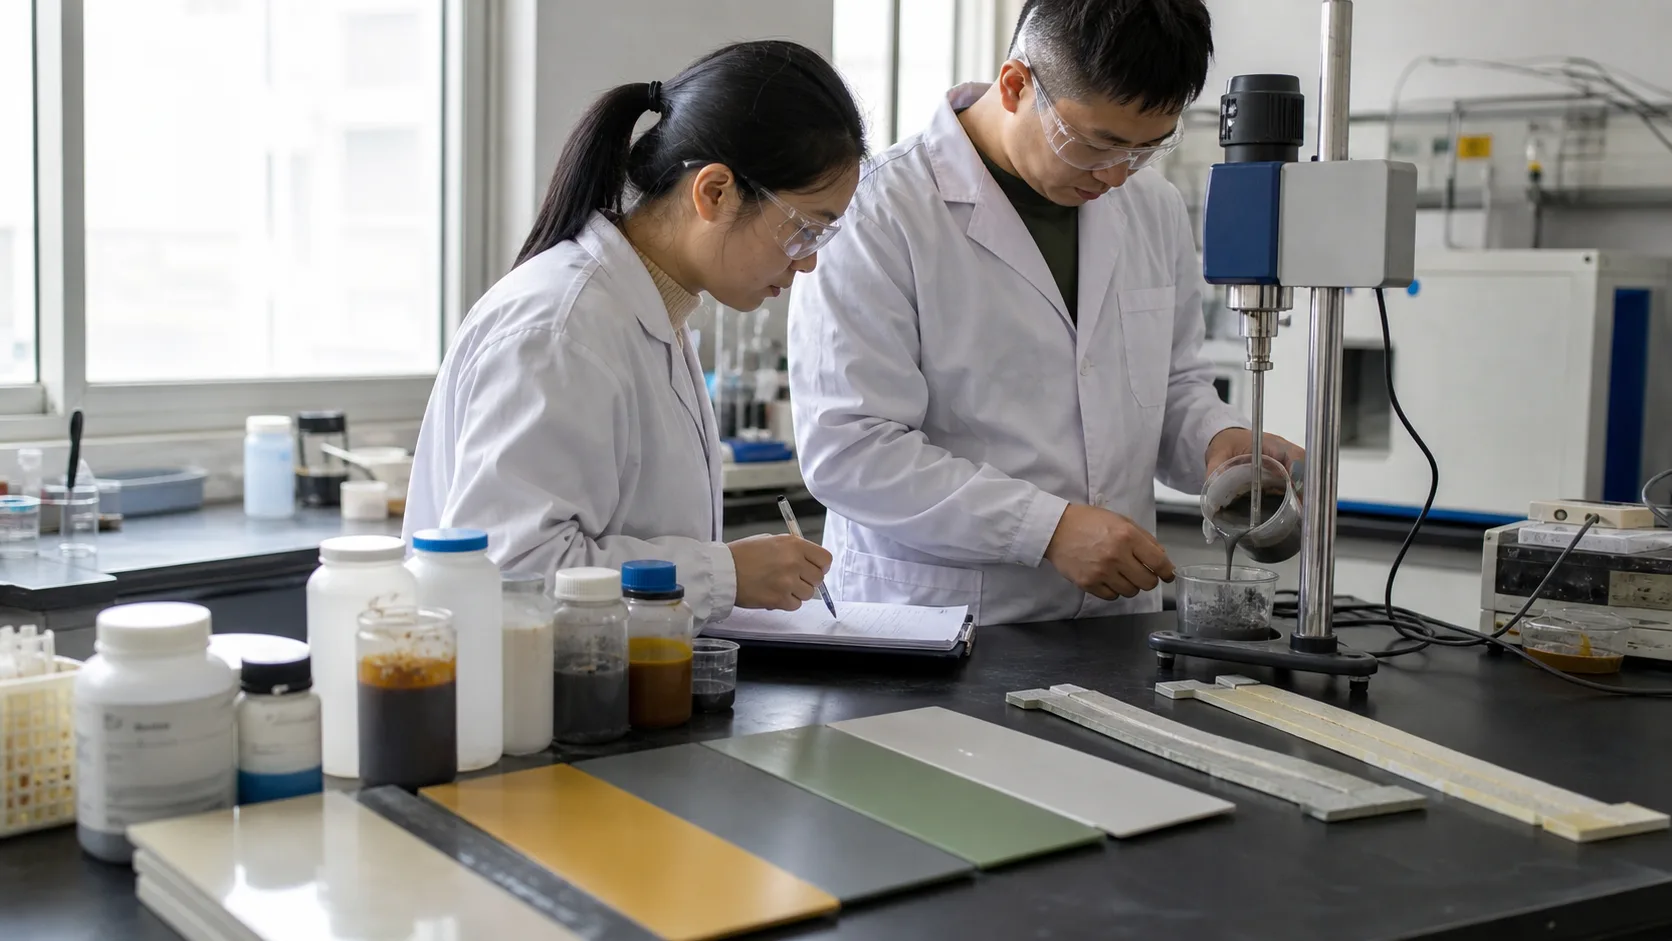
Laboratory staff examining coated panels beside testing equipment
Construction parameters
Viscosity affects suitability for rolling, troweling and spraying; solids content affects theoretical film yield; pot life and touch-dry time determine crew, tool and work-area planning. Compare parameters only at the same temperature and using the same test method.
Mechanicality and attachment
Assess adhesion in relation to substrate type, preparation and failure mode. Balance hardness, tensile strength, elongation and abrasion resistance; higher values are not always better for every application.
Weather and chemical resistance
For weathering tests, check the light source, cycle, duration, color change, gloss loss and chalking grade. For chemical resistance, specify the medium, concentration, temperature, contact method and duration.
At the procurement or design stage, prioritize test evidence that resembles the intended application instead of comparing a single number from promotional material.
Form project data sheets
Bring substrate conditions, application environment, target film thickness, recoat window, curing conditions and acceptance criteria together in one project data sheet so purchasing, application and inspection share the same requirements.
Establishing a comparable data base
Read the test method before comparing the number. Viscosity depends on temperature, spindle and speed; adhesion depends on substrate, preparation, test adhesive and pull rate. Hardness, tensile and abrasion results depend on specimen thickness and curing time. A procurement specification should state the method, specimen preparation, curing environment and acceptable range, and identify whether values refer to one component, the mixed material or the complete coating system.
Select parameters around equipment and the site work sequence. Lower viscosity improves penetration and leveling but may increase sagging; longer pot life aids large-area work but may delay access. High solids support film build but do not replace thickness control. Temperature affects mixed viscosity, reaction rate and air release, so typical data should not be treated as constant values under all conditions. Prepare sample panels across the intended temperature range.
From individual indicators to system balance
Assess hardness, flexibility, tensile strength and elongation together. Hardness can improve scratch resistance but may not suit moving substrates; high elongation accommodates crack movement, while heavy-duty floors also need modulus and abrasion resistance. In adhesion tests, identify whether failure occurs in the substrate, interface or coating. Concrete failure limits the result to substrate strength; clean intercoat separation points to the recoat window, contamination or incompatibility.
Evaluate color change, gloss loss, chalking, cracking and retained adhesion together. Chemical-resistance data must specify media, concentration, temperature, immersion or spot exposure and duration. Short-term stability does not establish long-term immersion suitability. Abrasion results depend on wheel type, load and cycles. Prioritize the relevant failure modes and balance secondary properties.
Forming a chain of project acceptance data
Translate laboratory parameters into practical site checks: mixed appearance, pot life, consumption per unit area, wet- and dry-film thickness, recoat time, return-to-service time, adhesion sampling and defect criteria. Define the instrument, frequency, locations and responsible person for each check. Retain batch, weighing, environmental and corrective-action records so final results can be traced to specific areas. A material pass certificate alone cannot explain local variations without process records.
Supplier documents, independent reports, site sample panels and completion testing serve different purposes: initial screening, performance under standard conditions, site suitability and delivered quality. They do not replace each other. For critical projects, agree witnessed sampling, retained samples, retesting and allowable tolerances in advance to support informed purchasing and consistent acceptance.
Project landing and risk review
Before work begins, the project lead should review site conditions with the designer, material supplier, applicator and owner, converting drawing requirements into an actionable area checklist. Include substrate type and condition, coating layers and thicknesses, details, material batches, mixing quantities, tools, crew responsibilities, environmental controls, recoat times and return-to-service conditions. Coordinate other trades, temporary power, ventilation, fire precautions and protection of completed work so that welding, cutting, dust and equipment installation do not interfere with coating. Inspect the first completed area and compare consumption and cure with the trial area before continuing at scale.
Use inspection hold points throughout the work instead of waiting until all surfaces are covered. Inspect and retain photographs and data after substrate preparation, primer sealing, defect repair, reinforcement of critical details and before final handover. If material condition, environmental limits, batch changes or widespread defects raise concerns, isolate the area, retain samples and records, and obtain a technical assessment. Every rework record should identify the failed interface, repair area, materials and retest results. Trial areas, witnessed process checks, traceable records and verified repairs help translate laboratory performance into reliable field performance.